


Weight
Low-density prints


Bambu Lab PLA Aero 1 kg with Spool
Low-density prints
Controlled foaming
RC aircraft components
| Material | PLA Aero 1 kg |
|---|---|
| Manufacturing process | FDM / FFF |
| Filament diameter | 1.75 mm |
| Net filament weight | 1 kg |
| Nozzle temperature | 210–260 °C |
| Bed temperature | 35–45 °C |
| Oven drying | 55 °C · 8 h |
| Recommended speed limit | < 180 mm/s |
Bambu Lab
The foaming formulation expands during extrusion to reduce the density of lightweight models such as RC aircraft components.
The foaming formulation expands during extrusion to reduce the density of lightweight models such as RC aircraft components.
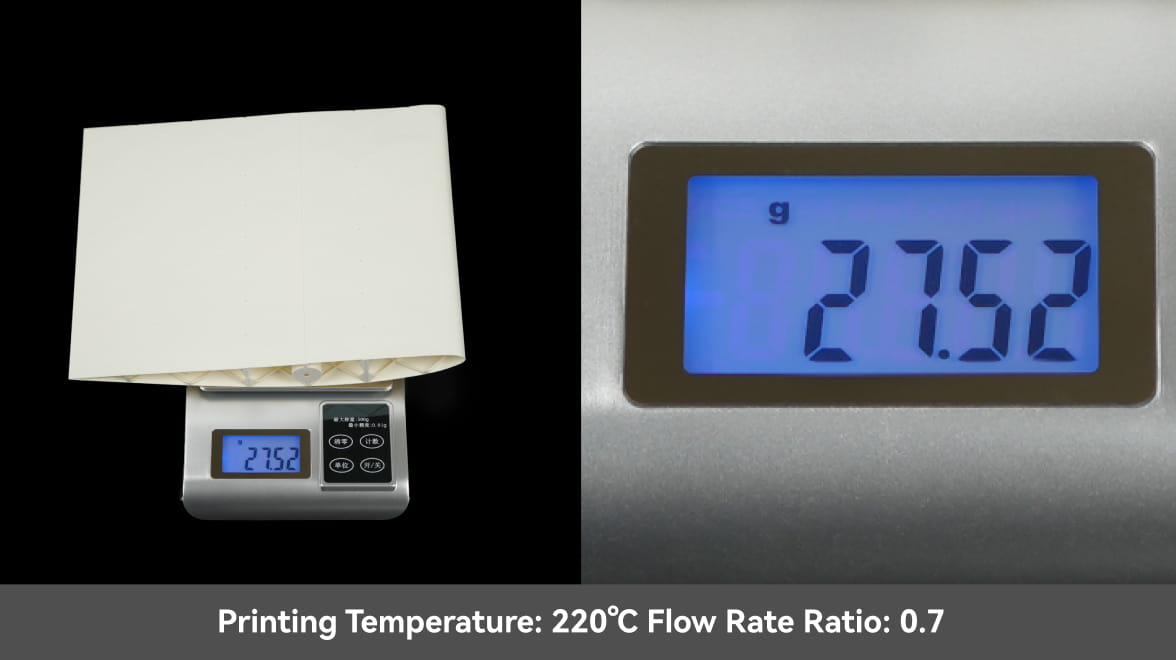
Temperature, flow ratio and geometry affect foaming and final density. Use the PLA Aero profile and calibrate before printing mating parts.
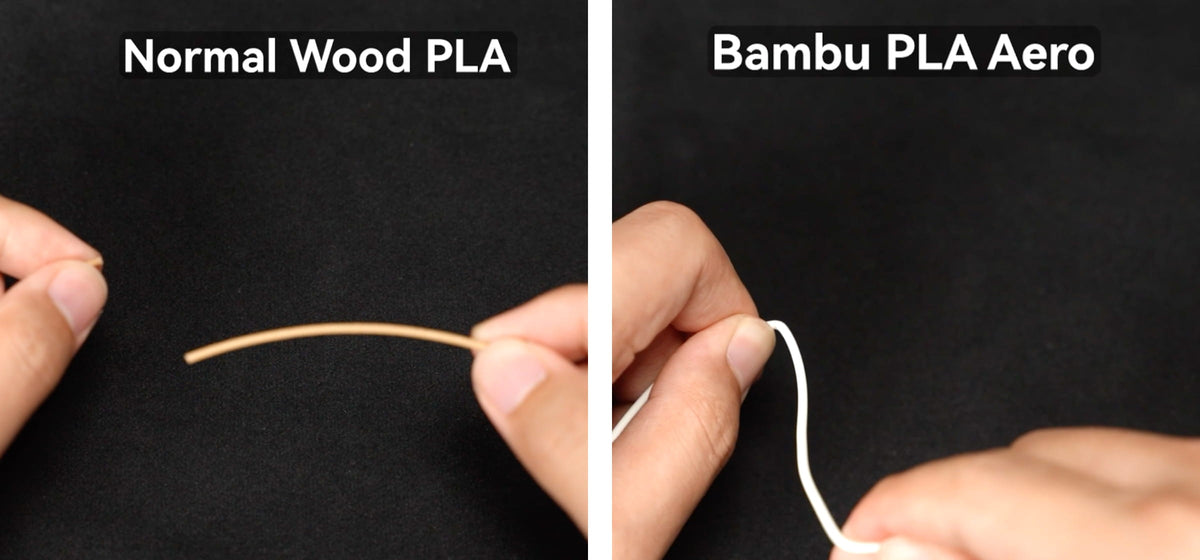
The supplier balances light weight and impact behaviour for model applications. Wall design still determines the strength of the part.
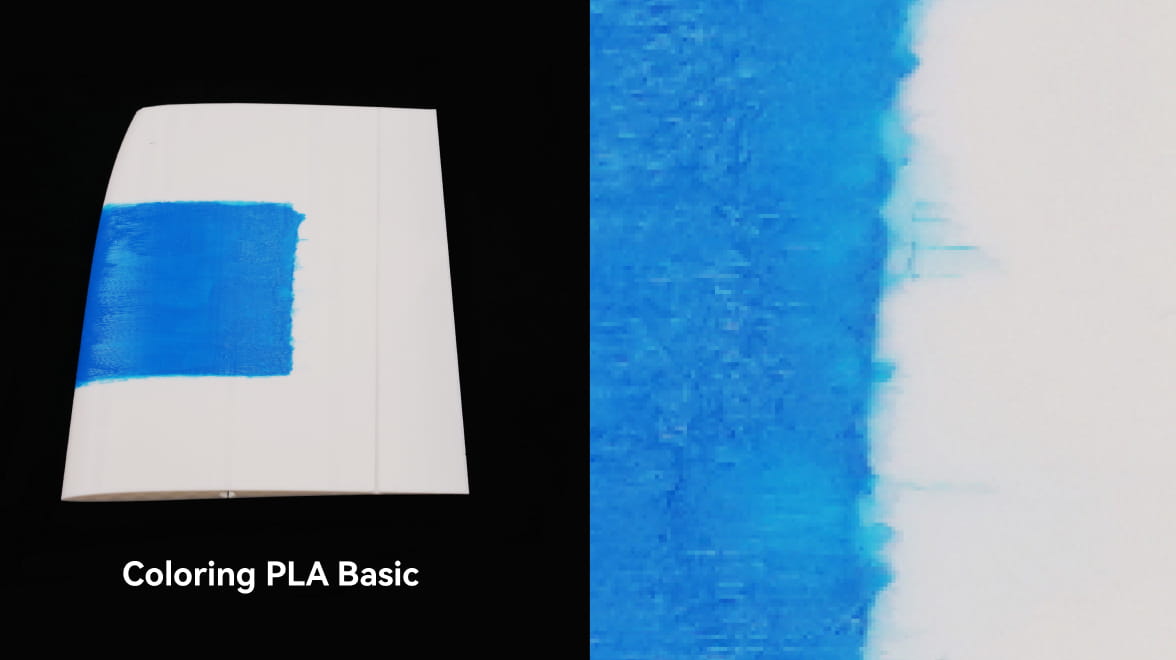
The matte surface is suited to colouring and finishing lightweight models. Test coating compatibility on a sample.
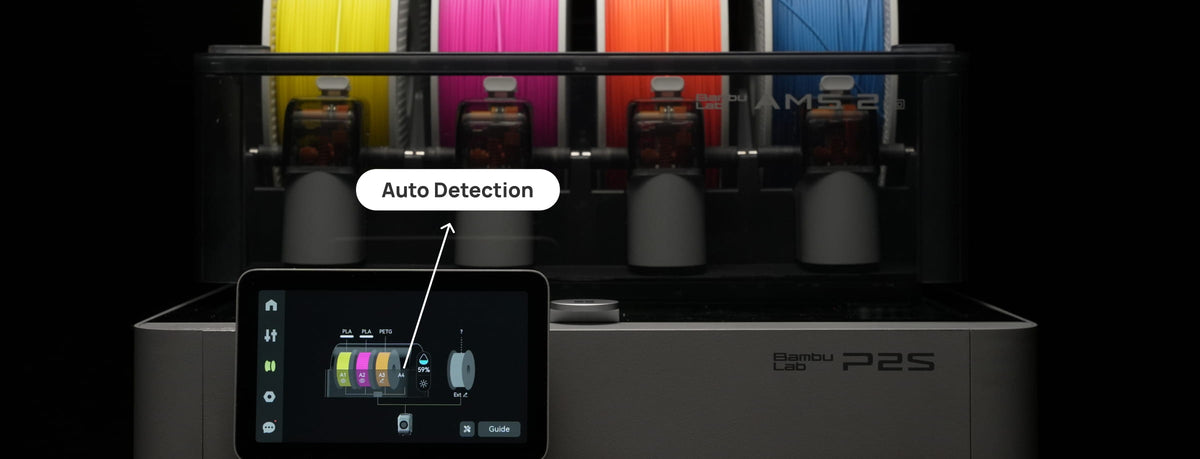
Compatible Bambu AMS systems identify the material from the spool RFID. Check the compatibility of the exact filament and feeding system.
Oven drying reference: 55 °C · 8 h. Keep the filament sealed with desiccant after drying. Follow the drying equipment guidance and the spool temperature limit.
Select the profile for this exact material. Print a sample to check surface finish, fit and adhesion before a larger batch.
1 filament spool in the selected colour and weight