


Reinforcement
Carbon fibres


Bambu Lab PETG-CF 1 kg with Spool
Carbon fibres
Increased bending resistance
Glossy composite texture
| Material | PETG-CF 1 kg |
|---|---|
| Manufacturing process | FDM / FFF |
| Filament diameter | 1.75 mm |
| Net filament weight | 1 kg |
| Nozzle temperature | 240–270 °C |
| Bed temperature | 65–75 °C |
| Oven drying | 65 °C · 8 h |
| Recommended speed limit | < 200 mm/s |
Bambu Lab
Carbon fibres reinforce PETG for functional parts that need to resist bending.
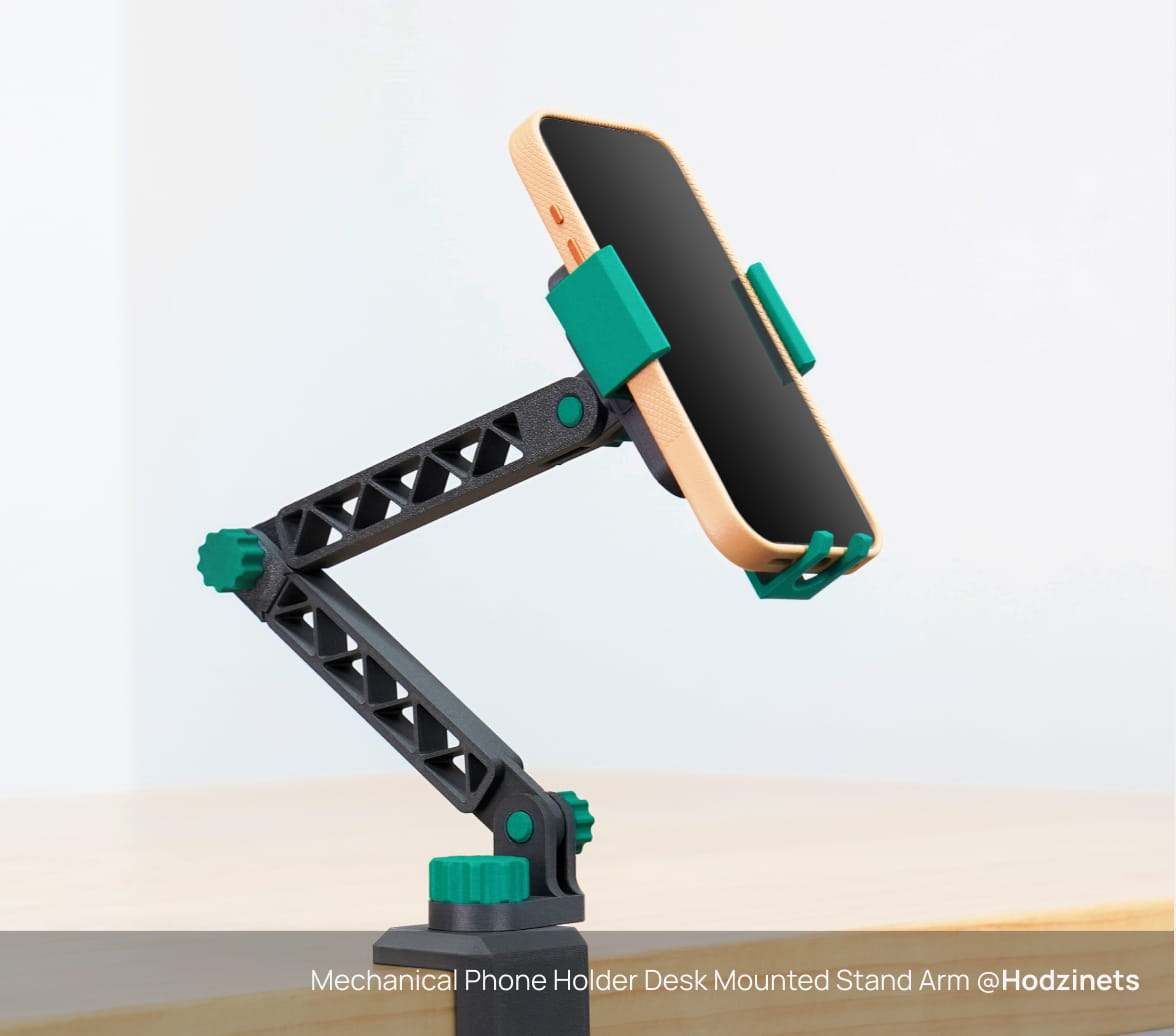
Carbon fibres reinforce PETG for functional parts that need to resist bending.

The supplier positions PETG-CF for outdoor accessories. Assess temperature, UV exposure and loading for the finished design.
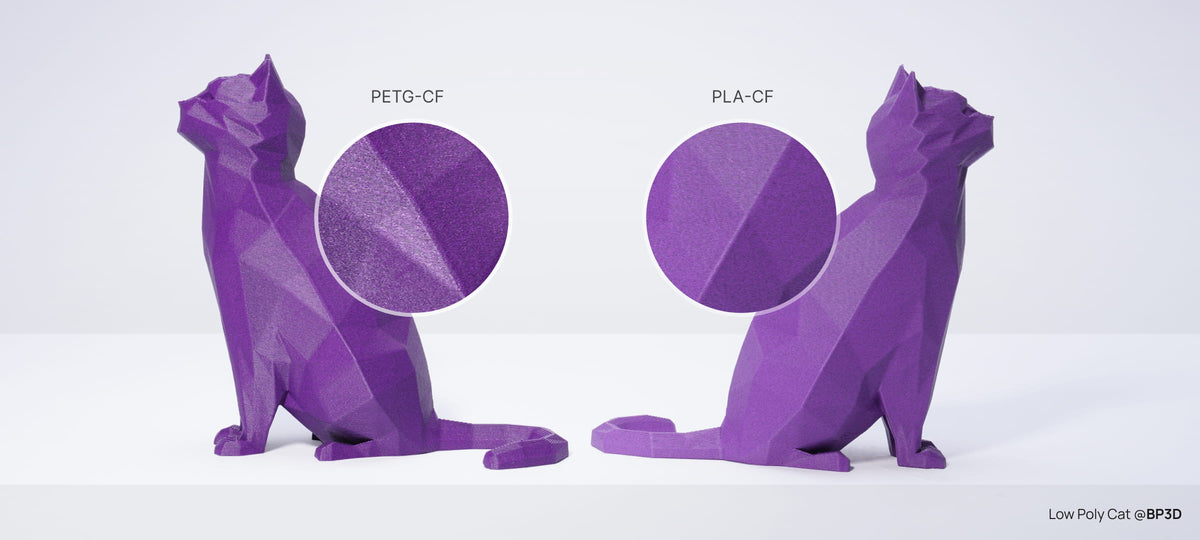
The carbon-filled surface combines a technical texture with a glossier appearance than many matte composites.
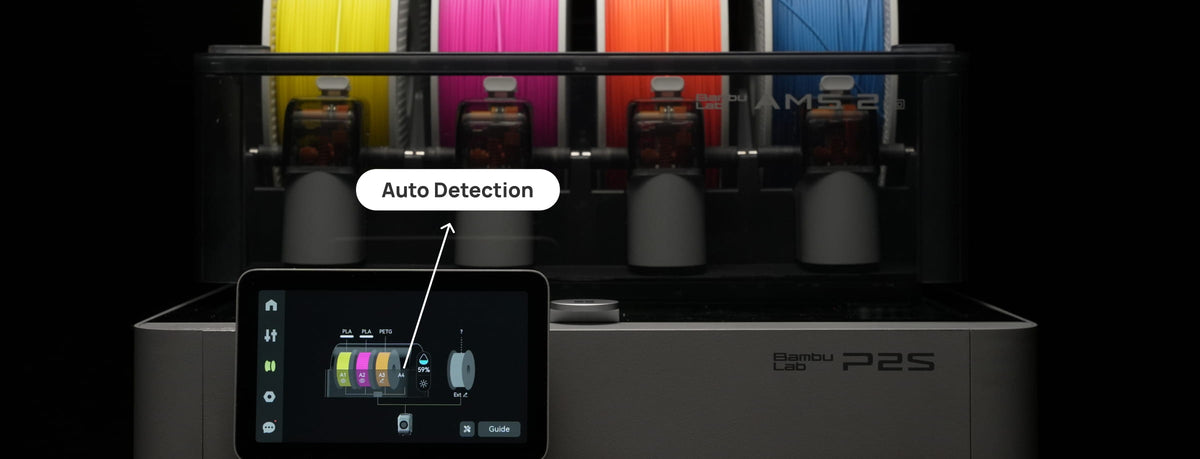
Compatible Bambu AMS systems identify the material from the spool RFID. Check the compatibility of the exact filament and feeding system.
Oven drying reference: 65 °C · 8 h. Keep the filament sealed with desiccant after drying. Follow the drying equipment guidance and the spool temperature limit.
Use a wear-resistant nozzle and verify the printer temperature capability. Dry the composite before printing and validate part orientation for the expected loads.
1 filament spool in the selected colour and weight